At ARZAAQ, manufacturing excellence is built on advanced technology, rigorous process control, and an unwavering commitment to operational performance. Our integrated production capabilities are designed to deliver premium ready-to-eat meals that combine exceptional quality, extended shelf life, and consistent reliability.
Production technology
Advanced manufacturing technology
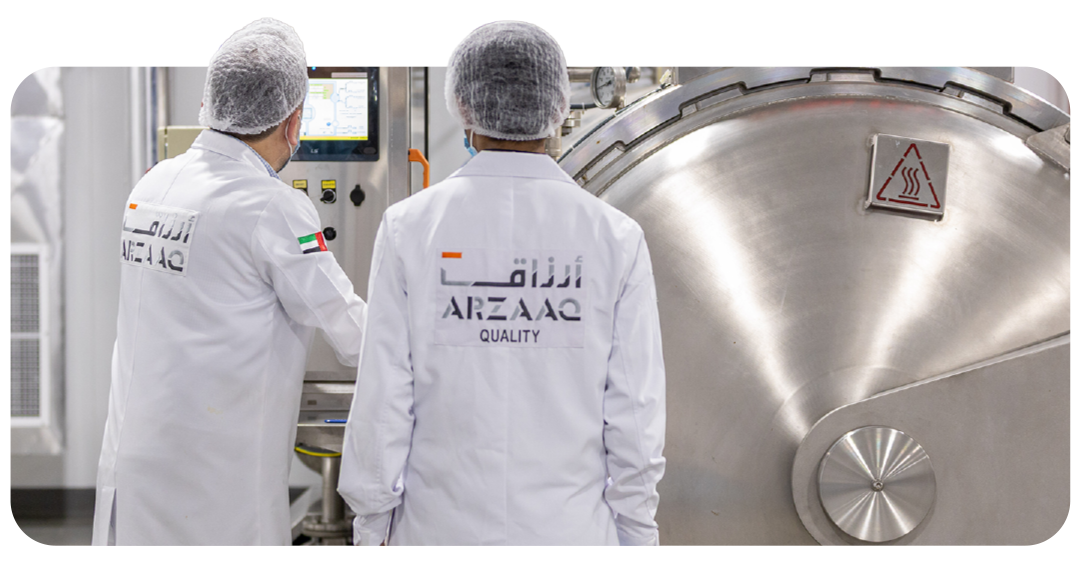
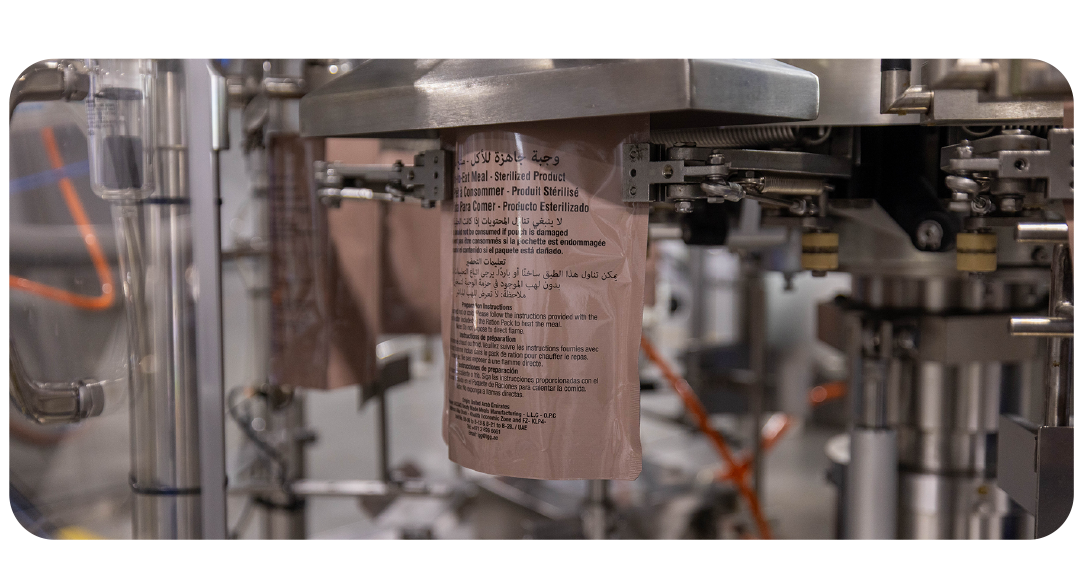
State-of-the-art production facilities equipped with steam cooking, controlled drying, automated pouch filling and sealing, and high-pressure autoclave sterilization to ensure product safety, consistency, and efficiency.
Precision-driven production
Standardized manufacturing processes and automated systems deliver uniform quality, taste, texture, and nutritional value across every production batch.
Operational excellence
Lean manufacturing principles maximize productivity, optimize resources, and enhance production efficiency while minimizing waste.
Innovation in food solutions
Continuous product development creates nutritious, ready-to-eat meal solutions with an extended shelf life of up to 2–3 years without compromising taste, quality, or nutritional integrity.
Advanced packaging technology
High-performance packaging protects against oxygen, moisture, and light, preserving freshness and ensuring product stability throughout storage, transportation, and distribution.
Reliable supply chain
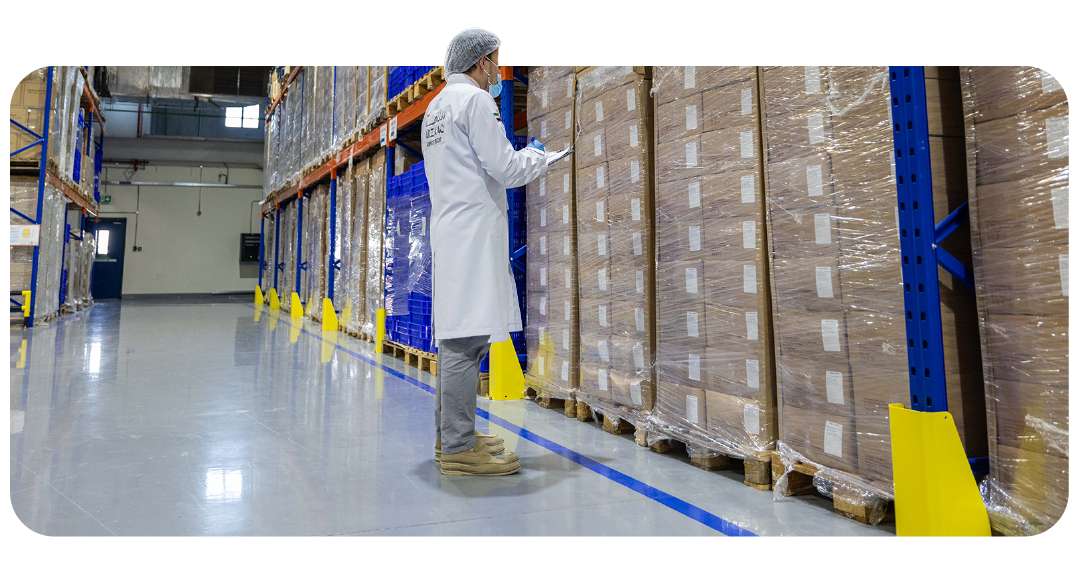
Strategic sourcing, robust production planning, and dependable inventory management ensure uninterrupted supply and consistent delivery to customers across diverse commercial markets.
Assurance & standards
Quality excellence
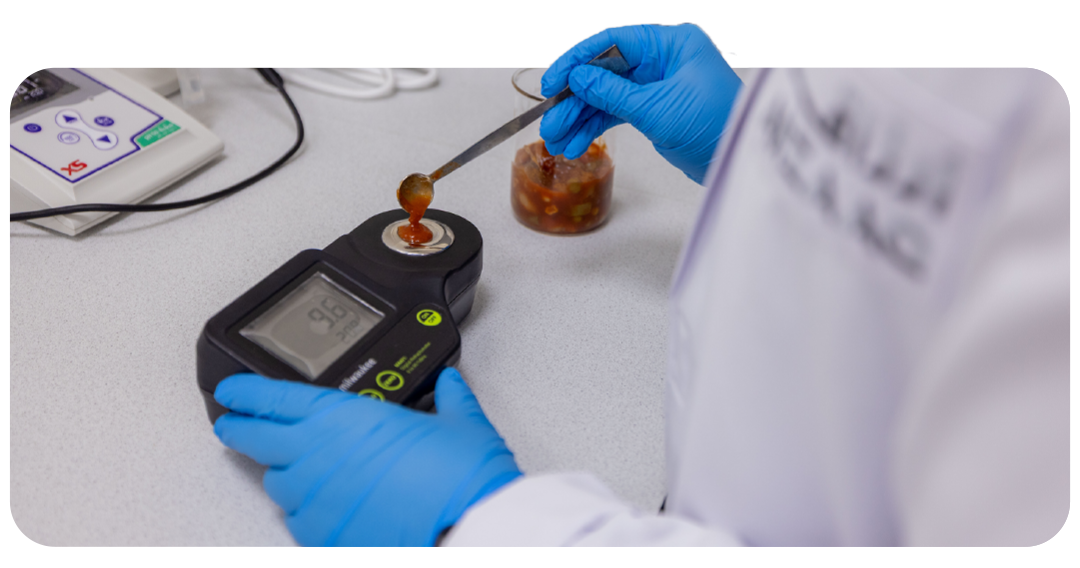
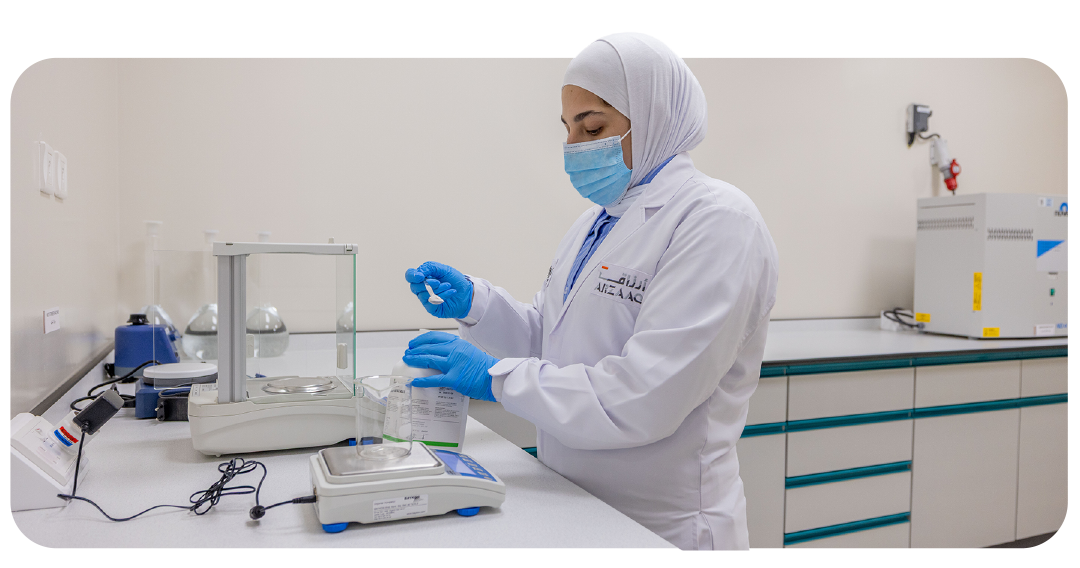
Quality is embedded into every stage of our operations. From supplier qualification to final product release, ARZAAQ applies comprehensive quality assurance systems that ensure every product meets the highest standards of food safety, consistency, and customer satisfaction.
Global food safety standards

Manufacturing operations are aligned with internationally recognized food safety and quality management systems, ensuring products consistently meet global industry expectations.
Comprehensive quality assurance

Multi-stage inspections and verification processes are conducted throughout raw material receipt, production, packaging, and final product release to maintain uncompromising quality.
End-to-end traceability

Fully integrated batch traceability enables complete visibility from approved raw materials to finished products, ensuring transparency, accountability, and rapid response capabilities.
Shelf-life validation

Extensive stability studies and quality verification programs confirm product safety, nutritional value, and sensory performance throughout their intended shelf life.
Regulatory excellence

Full compliance with applicable food safety regulations and quality requirements ensures products that are safe, reliable, and consistently manufactured.
Culture of continuous improvement

Performance analytics, customer insights, and ongoing process optimization drive continuous innovation, operational excellence, and sustained product enhancement.
Reach out to us
Arrange a technical discussion
Our production and quality teams are glad to walk through process, specification and validation in detail.